Procurement Reference
PPAP for sheet metal contract manufacturing
What a PPAP submission for a sheet metal part contains — the AIAG elements, submission levels 1–5, what a fabricator can realistically supply, resubmission triggers, and how it differs from FAI.
By Nevatronix Sheet Metal 10 min read
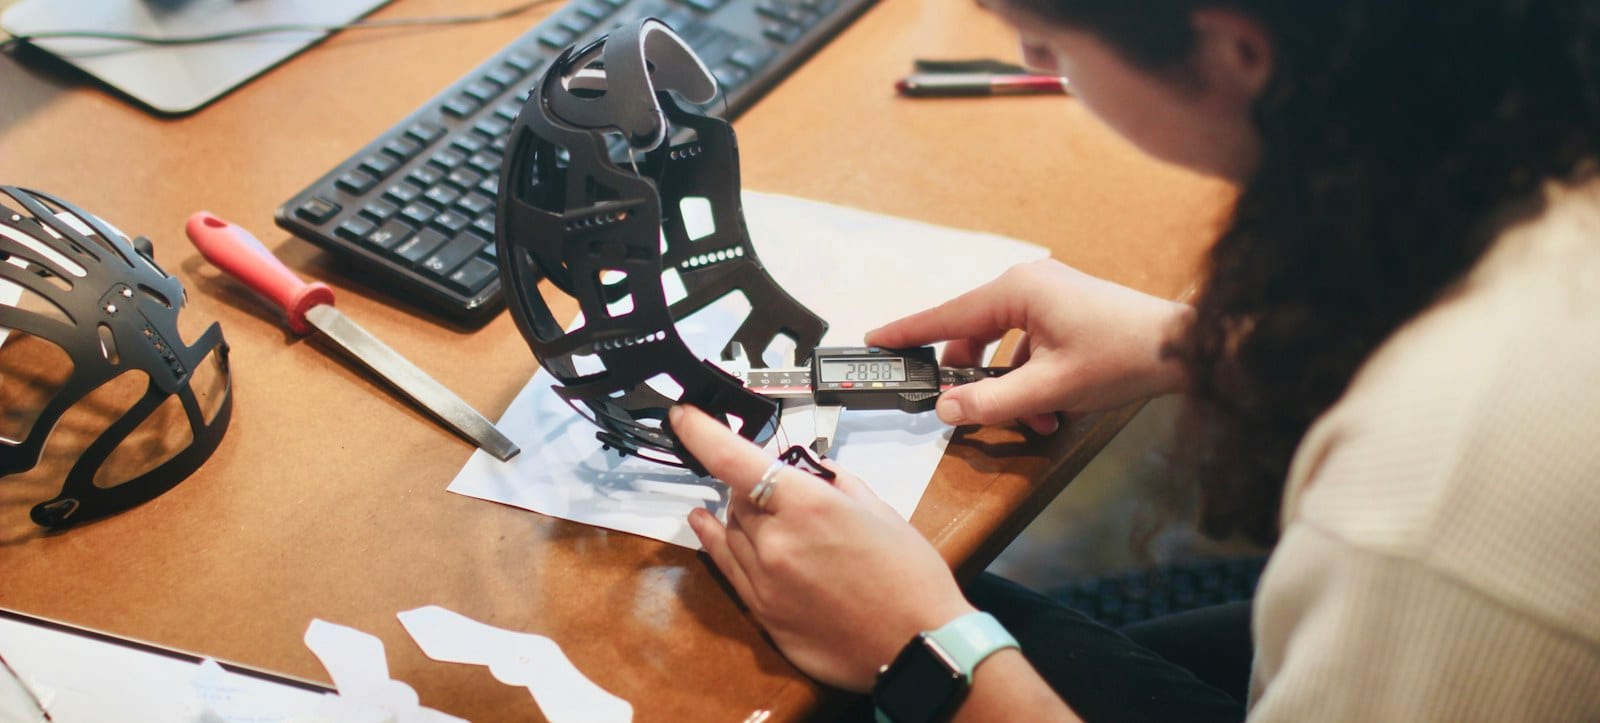
A PPAP (Production Part Approval Process) submission for a sheet metal part is the documentation package that proves a fabricator’s production process can make that part to the drawing, repeatably, at rate. It bundles the design record, process flow, PFMEA, control plan, measurement studies, a ballooned dimensional report, material certs, capability data, sample parts, and a signed warrant.
What is PPAP actually for?
PPAP is a format defined by the Automotive Industry Action Group (AIAG). It grew up in the automotive supply chain, where IATF 16949 makes it mandatory, but it has spread to anyone who buys production parts and wants more than a first-article report: gaming cabinet OEMs, ATM and cash-handling manufacturers, kiosk builders.
The distinction that matters to a procurement engineer: a first article answers “does this part match the drawing?” A PPAP answers “do you understand and control the process well enough that the ten-thousandth part will match too?” The dimensional report inside a PPAP is only one of its elements; the rest of the package is about the process.
One thing to say plainly up front. Nevatronix Sheet Metal is certified to ISO 9001:2015. We are not certified to IATF 16949 and do not claim to be. A PPAP is a document set, not a certification, and an ISO 9001 shop with a working quality system can produce one. We support PPAP submissions when a customer’s program calls for them.
The PPAP elements and what they mean on a sheet metal part
The AIAG manual (4th edition) lists 18 elements. Not all of them apply to every part, and not all are supplied by the fabricator. The table maps each one onto a typical build-to-print sheet metal part.
| # | PPAP element | What it is on a sheet metal part | Who supplies it |
|---|---|---|---|
| 1 | Design record | Released drawing, CAD (STEP/DXF), material and finish spec, revision level | Customer; fabricator confirms the revision built |
| 2 | Authorized engineering change documents | Any deviation or ECN not yet on the drawing | Customer |
| 3 | Customer engineering approval | Sign-off that samples met engineering’s needs | Customer |
| 4 | Design FMEA | Failure-mode analysis of the design itself | Customer (design owner) |
| 5 | Process flow diagram | Cut → deburr → form → hardware → weld → finish → assemble → inspect → pack | Fabricator |
| 6 | Process FMEA | Failure modes at each step (mis-bend, missed hardware, coating thickness) with controls | Fabricator |
| 7 | Control plan | What is checked, how, how often, and what happens on a failure | Fabricator |
| 8 | Measurement system analysis | Gauge R&R on the calipers, height gauges, angle gauges, CMM used in the control plan | Fabricator |
| 9 | Dimensional results | Ballooned drawing plus a results sheet for every feature, on the sample lot | Fabricator |
| 10 | Material and performance test results | Mill certs, coating thickness, salt-spray or adhesion where specified | Fabricator (mill and finisher certs attached) |
| 11 | Initial process studies | Short-run capability on designated critical features | Fabricator |
| 12 | Qualified laboratory documentation | Accreditation of any outside lab used for testing | Third-party lab |
| 13 | Appearance approval report | Color, gloss, texture sign-off on cosmetic parts | Fabricator prepares; customer signs |
| 14 | Sample production parts | Parts from the actual production process | Fabricator |
| 15 | Master sample | A retained, signed reference part | Fabricator retains |
| 16 | Checking aids | Fixtures, go/no-go gauges, templates specific to the part | Fabricator (if any exist) |
| 17 | Customer-specific requirements | Anything the customer’s supplier manual adds | Both |
| 18 | Part Submission Warrant (PSW) | The signed cover sheet declaring the part and process approved for production | Fabricator signs; customer countersigns |
For a build-to-print part the design-side elements (1–4) are the customer’s, the process-side elements (5–11, 14–16, 18) are the fabricator’s, and 12, 13, and 17 depend on third parties or the customer’s supplier manual.
Submission levels 1–5: what actually gets sent
The level is set by the customer, and it controls what is submitted versus what is retained at the supplier and available on request. The elements exist at every level; the level changes where they live.
| Level | What is submitted to the customer | Typical use |
|---|---|---|
| 1 | Warrant only (plus appearance approval report for appearance items) | Low-risk parts, re-qualification after a minor change |
| 2 | Warrant, sample parts, limited supporting data | Parts with a short history of conforming production |
| 3 | Warrant, sample parts, complete supporting data | The default when no level is specified |
| 4 | Warrant plus whatever the customer specifically lists | Customer-defined packages |
| 5 | Warrant, sample parts, complete data — reviewed at the supplier’s plant | New suppliers, high-risk parts, on-site audits |
Assume Level 3 if a supplier manual says “PPAP required” and nothing else. If your program only needs the warrant and a dimensional report, say Level 1 or 2 on the purchase order; it removes days of documentation work from the quote without removing evidence you would read.
What does the dimensional report look like?
Element 9 is the same ballooned report a first article uses. Every dimension, note, and GD&T callout on the drawing gets a balloon number; the results sheet lists nominal, tolerance, the measured value on each sample, the instrument, and pass/fail.
On sheet metal the values are what the process holds: laser-cut and punched feature-to-feature positions in the ±0.1 mm (±0.004 in) range, bend angles ±0.5°, dimensions across a bend ±0.2–0.5 mm. The full set is in our sheet metal tolerance reference; the drawing’s general block (ISO 2768-m is the sensible default) decides how many balloons carry a specific tolerance.
Two details that save a resubmission cycle:
- The report is against the revision on the PSW. If a redline exists, it either goes into element 2 as an authorized change or the drawing gets rolled before the PPAP is built. A report against a superseded revision is rejected on receipt.
- Number of samples. The AIAG manual does not fix a sample count; customer supplier manuals do. Five is common for the dimensional layout, with a larger sample (often 25–30 pieces or more) only for the capability study in element 11.
Capability, MSA, and the control plan
These three elements are what separate a PPAP from an FAI, and they are where a sheet metal fabricator has to be realistic about what can be studied.
Initial process studies (element 11). A capability study needs a variable measurement on a run of parts, so it is done on designated features: a critical hole position, a formed height, a bend angle on a mating flange, a coating thickness. The AIAG manual’s acceptance criterion is commonly summarized as: an index of 1.67 or above meets the requirement; 1.33–1.67 may be accepted with customer agreement and added controls; below 1.33 does not. The customer designates the features on the drawing or in the supplier manual; if none are designated, ask before running 30 parts across a CMM for a study nobody requested.
Measurement system analysis (element 8). A gauge R&R study on the instruments named in the control plan. The AIAG MSA guidelines commonly applied: under 10% of tolerance consumed by gauge variation is acceptable, 10–30% marginal, above 30% not acceptable. Calipers on a ±0.5 mm dimension pass easily; calipers on a ±0.05 mm dimension do not, which is one more reason a ±0.05 mm callout costs money — it forces a CMM into the control plan and an MSA study onto the CMM.
Control plan (element 7). The document a customer auditor actually reads. Per operation it lists the characteristic checked, the specification, the instrument, the sample size and frequency (first article plus every n pieces), and the reaction plan on a nonconformance. Our production programs already run first-article-then-sample-inspect under ISO 9001; the control plan is that pattern written against the customer’s format, with the press brake cell’s inspection sign-off and assembly lot serialization mapped onto it.
What triggers a resubmission?
A PPAP approves a specific part made by a specific process. Change either and the approval no longer applies. The triggers the AIAG manual lists, translated to a fabricator:
- Drawing revision, material change, or finish change on the part.
- New, replacement, or refurbished tooling — for sheet metal this mostly means new forming fixtures, weld fixtures, or checking aids, since brake dies and laser programs are not part-specific tooling in the automotive sense.
- A new machine, a moved machine, or a changed process step — for example moving a weld from a manual bay to a robotic cell, or changing the order of forming and hardware insertion.
- A change of sub-tier supplier — a different mill source is usually fine with a new cert, but a different plating, anodizing, or e-coat house is a resubmission trigger, because the finish process changed.
- Production moving to a different site.
- Tooling idle for twelve months or more before the next order.
The supplier’s obligation is to notify before shipping changed parts; the customer decides whether a full Level 3 or a reduced Level 1 resubmission is required. Most running changes on a sheet metal part — a bend sequence tweak, a nest change — do not alter the part and trigger nothing. A material substitution or a finisher change always does.
How PPAP differs from FAI
The two terms get used interchangeably, and it changes the quote.
| First article inspection (FAI) | PPAP | |
|---|---|---|
| Question answered | Does this part match the drawing? | Can the process make this part repeatably? |
| Core content | Ballooned dimensional report, material certs | Everything in an FAI plus process flow, PFMEA, control plan, MSA, capability, warrant |
| Sample basis | One part (sometimes three) from the production process | Sample lot plus a capability run on designated features |
| Format | Often the aerospace FAI form format, which non-aerospace shops borrow | AIAG PPAP forms and the PSW |
| Repeated when | First run, and after any change affecting form/fit/function | Same triggers, plus process and sub-tier changes |
| Typical effort | Hours to a day of inspection | Days of documentation on top of the inspection |
Every production order at Nevatronix opens with a documented first article under ISO 9001 whether or not the customer asks. A PPAP is that first article plus the process documentation around it, quoted as a separate line because the PFMEA, control plan, and capability run are real engineering hours. If you only need to know the part matches the drawing, an FAI is the right ask and the cheaper one.
Where this breaks down
PPAP was written for automotive part families on dedicated tooling, and some of it maps poorly onto job-shop sheet metal:
- “Tooling” means something different. A press brake die set and a laser program are not part-specific tooling; a tooling-change trigger has to be interpreted as fixtures and checking aids.
- Capability on a 25-piece order is statistically thin. A study wants 30-plus parts; a pilot run may not have them. Low-volume customers usually waive element 11 or defer it to the first production lot — agree that on the PO.
- Partner finishes are outside our process. Anodize, plating, e-coat, and wet paint run through managed partners. We attach their certifications and coating reports, but we cannot write a PFMEA for a plating line we do not operate. In-house powder coat is fully inside the package.
- Design-side elements are not ours to write. On a build-to-print part the DFMEA and engineering approval are the customer’s; a request that expects the fabricator to supply them stalls.
- We do not take work that needs AS9100, ISO 13485, or ITAR registration. Programs that need those certifications alongside PPAP should qualify a supplier that holds them.
What to put on the drawing or RFQ
To get a usable PPAP quote instead of a question back:
- State the submission level (1–5). If unsure, Level 3.
- Reference the supplier manual or attach the forms you want used, and say whether AIAG forms are acceptable.
- Designate the critical characteristics for the capability study on the drawing, and state the sample size and the index required.
- Specify the material and finish by standard (for example ASTM A1008 CS Type B, powder coat to a named color and thickness) so element 10 has something to certify against.
- Say what triggers you consider a resubmission, especially for sub-tier finishers, and whether a reduced resubmission is acceptable.
- Separate FAI from PPAP in the RFQ so the two are quoted as different lines.
How we’d quote your part
Send the drawing, CAD, quantity, and your supplier manual or PPAP level to our quote page. We build the process flow, PFMEA, control plan, and dimensional report against your format, run the capability study on the features you designate, and sign the warrant under our ISO 9001:2015 system. If your program needs IATF 16949 or a regulated-industry certification, we will say so and not quote it.
References
- AIAG — Production Part Approval Process (PPAP) manual, 4th edition
- AIAG — Quality core tools (APQP, PPAP, FMEA, MSA, SPC) overview
- IATF Global Oversight — IATF 16949 automotive quality management standard
- ASME Y14.5 — Dimensioning and tolerancing (the basis for the ballooned dimensional report)
- NIST Statistical Engineering Division — measurement uncertainty and process statistics
- ASTM A1008/A1008M — Cold-rolled carbon steel sheet (the specification a mill cert references)
Frequently asked questions
- What does a PPAP submission for a sheet metal part include?
- A Level 3 PPAP for a sheet metal part typically bundles the design record (the released drawing and CAD), a process flow diagram, a PFMEA, a control plan, gauge R&R studies for the measuring equipment, a ballooned dimensional report against every drawing feature, mill material certifications, initial process capability on the critical features, sample parts, and the signed Part Submission Warrant. The customer's submission level decides which of those are sent versus kept on file at the supplier.
- What are the five PPAP submission levels?
- Level 1 is the warrant only (plus an appearance report if the part is an appearance item). Level 2 is the warrant with sample parts and limited supporting data. Level 3 is the warrant with sample parts and the complete data package, and is the default when a customer does not specify. Level 4 is the warrant plus whatever the customer specifically lists. Level 5 is the full package, but reviewed at the supplier's plant instead of shipped.
- Does a sheet metal fabricator need IATF 16949 to submit a PPAP?
- No. PPAP is a document format defined by AIAG, and any supplier with a functioning quality system can produce one. IATF 16949 is the automotive management-system certification that makes PPAP mandatory for its supply chain. Nevatronix is certified to ISO 9001:2015, not IATF 16949, and supports PPAP submissions when a customer's program requires them.
- What is the difference between PPAP and FAI?
- A first article inspection verifies that one part, made by the production process, matches every dimension and note on the drawing. A PPAP verifies that the process itself is understood, controlled, and capable of making that part at rate — it contains an FAI-style dimensional report as one of its elements, plus the process flow, PFMEA, control plan, measurement studies, and capability data that FAI never asks for.
- What changes trigger a PPAP resubmission?
- Anything that changes the part or the process that makes it: a drawing revision or material change, new or refurbished tooling, a new or relocated machine or process step, a change of sub-tier supplier such as a plating or powder coat house, production moving to a different site, or tooling that has sat idle for a year or more. The customer decides whether the resubmission is a full package or a reduced one; the supplier's job is to notify before the change ships.
- What capability index does a PPAP ask for on a sheet metal feature?
- The AIAG PPAP manual's initial process study criterion is commonly summarized as an index of 1.67 or higher meeting the requirement, 1.33 to 1.67 possibly acceptable with customer agreement and added controls, and below 1.33 not meeting it. On a sheet metal part that study is usually run on a few designated critical features — a hole position, a formed height, a bend angle — not on every dimension.
- Which PPAP elements can a fabricator not supply on its own?
- The design FMEA belongs to whoever owns the design, which is the customer for a build-to-print part. Customer engineering approval and appearance approval need the customer's signature. Test results from outside laboratories, and certifications from partner finishers such as anodizing or plating houses, come from those third parties and are passed through with their documentation attached.